Acrylate Monomers Factory Solutions

All Categories

acrylate monomers factory

An acrylate monomers factory is a specialized manufacturing facility dedicated to producing high-quality acrylate-based chemical compounds used across numerous industries worldwide. These production plants synthesize various acrylate monomers through controlled chemical processes, including methyl acrylate, ethyl acrylate, butyl acrylate, and 2-ethylhexyl acrylate. The main functions of an acrylate monomers factory encompass raw material processing, polymerization reactions, purification procedures, quality control testing, and safe packaging for distribution. Advanced production technologies employed in these facilities include continuous reactor systems, distillation towers, automated monitoring equipment, and strict environmental control mechanisms that ensure consistent product quality and safety standards. The technological features of modern facilities incorporate energy-efficient processing methods, waste reduction systems, real-time quality monitoring, and compliance with international safety regulations. Applications of products manufactured in an acrylate monomers factory span multiple sectors including adhesives manufacturing, coating formulations, textile treatments, plastic modification, paint production, printing inks, and construction materials. These versatile chemical building blocks serve as essential raw materials for producing polymers and copolymers that exhibit excellent adhesion properties, weather resistance, flexibility, and durability. The strategic importance of an acrylate monomers factory lies in its ability to supply consistent, high-purity materials that meet stringent industry specifications while maintaining cost-effectiveness and environmental responsibility throughout the manufacturing process.
Popular Products

Choosing products from a reputable acrylate monomers factory delivers substantial practical benefits that directly impact your bottom line and operational efficiency. Production facilities with advanced manufacturing capabilities ensure you receive materials with consistent purity levels, reducing formulation variations and production waste in your downstream processes. This consistency translates to predictable performance in your final products, whether you manufacture adhesives, coatings, or specialty polymers. The operational benefits include reliable supply chains that minimize production interruptions, technical support from experienced chemical engineers who understand your application requirements, and flexible ordering quantities that align with your inventory management strategies. A well-established acrylate monomers factory maintains rigorous quality control protocols, providing you with certified materials that meet international standards such as ISO certifications and industry-specific compliance requirements. This eliminates costly quality issues and simplifies your regulatory documentation processes. Application suitability is another crucial advantage, as specialized facilities can customize monomer specifications to match your exact formulation needs, whether you require specific molecular weights, purity grades, or additive packages. Cost efficiency emerges through economies of scale that modern facilities achieve, passing savings to customers through competitive pricing while maintaining superior quality standards. Environmental responsibility increasingly matters to businesses, and leading factories implement sustainable practices including waste recycling, emission controls, and energy optimization that support your corporate sustainability goals. Partnership with an established acrylate monomers factory provides decision-useful context through market insights, technical documentation, application development support, and long-term supply agreements that protect against market volatility. These combined advantages create measurable value by reducing your total cost of ownership, improving product performance, accelerating time-to-market, and strengthening your competitive position in demanding markets.

Tips And Tricks

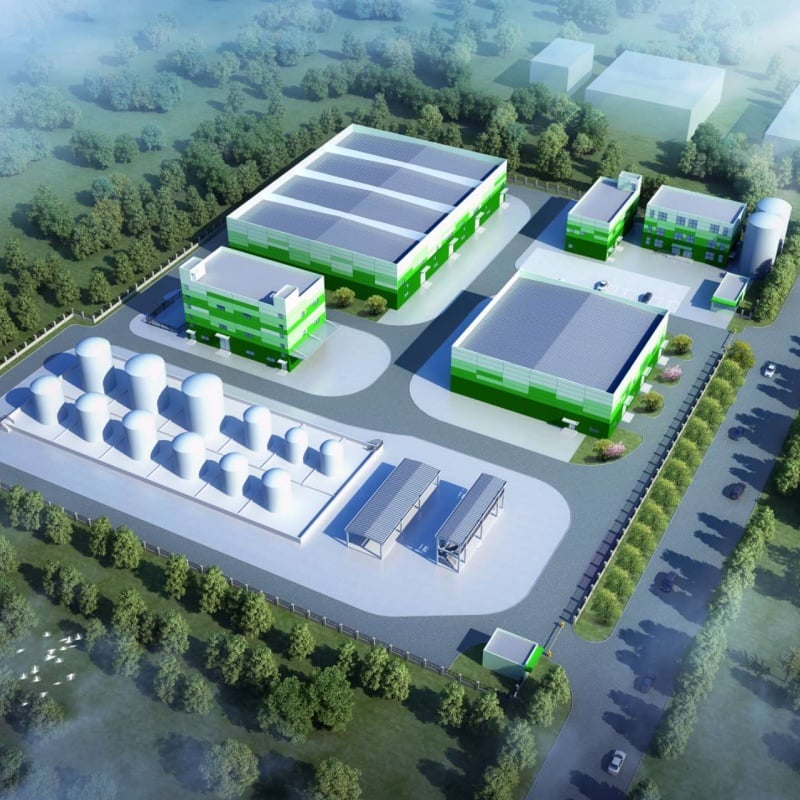
New Tank Farm Project to Boost Domestic and International Trade

18

Apr

New Tank Farm Project to Boost Domestic and International Trade

View More
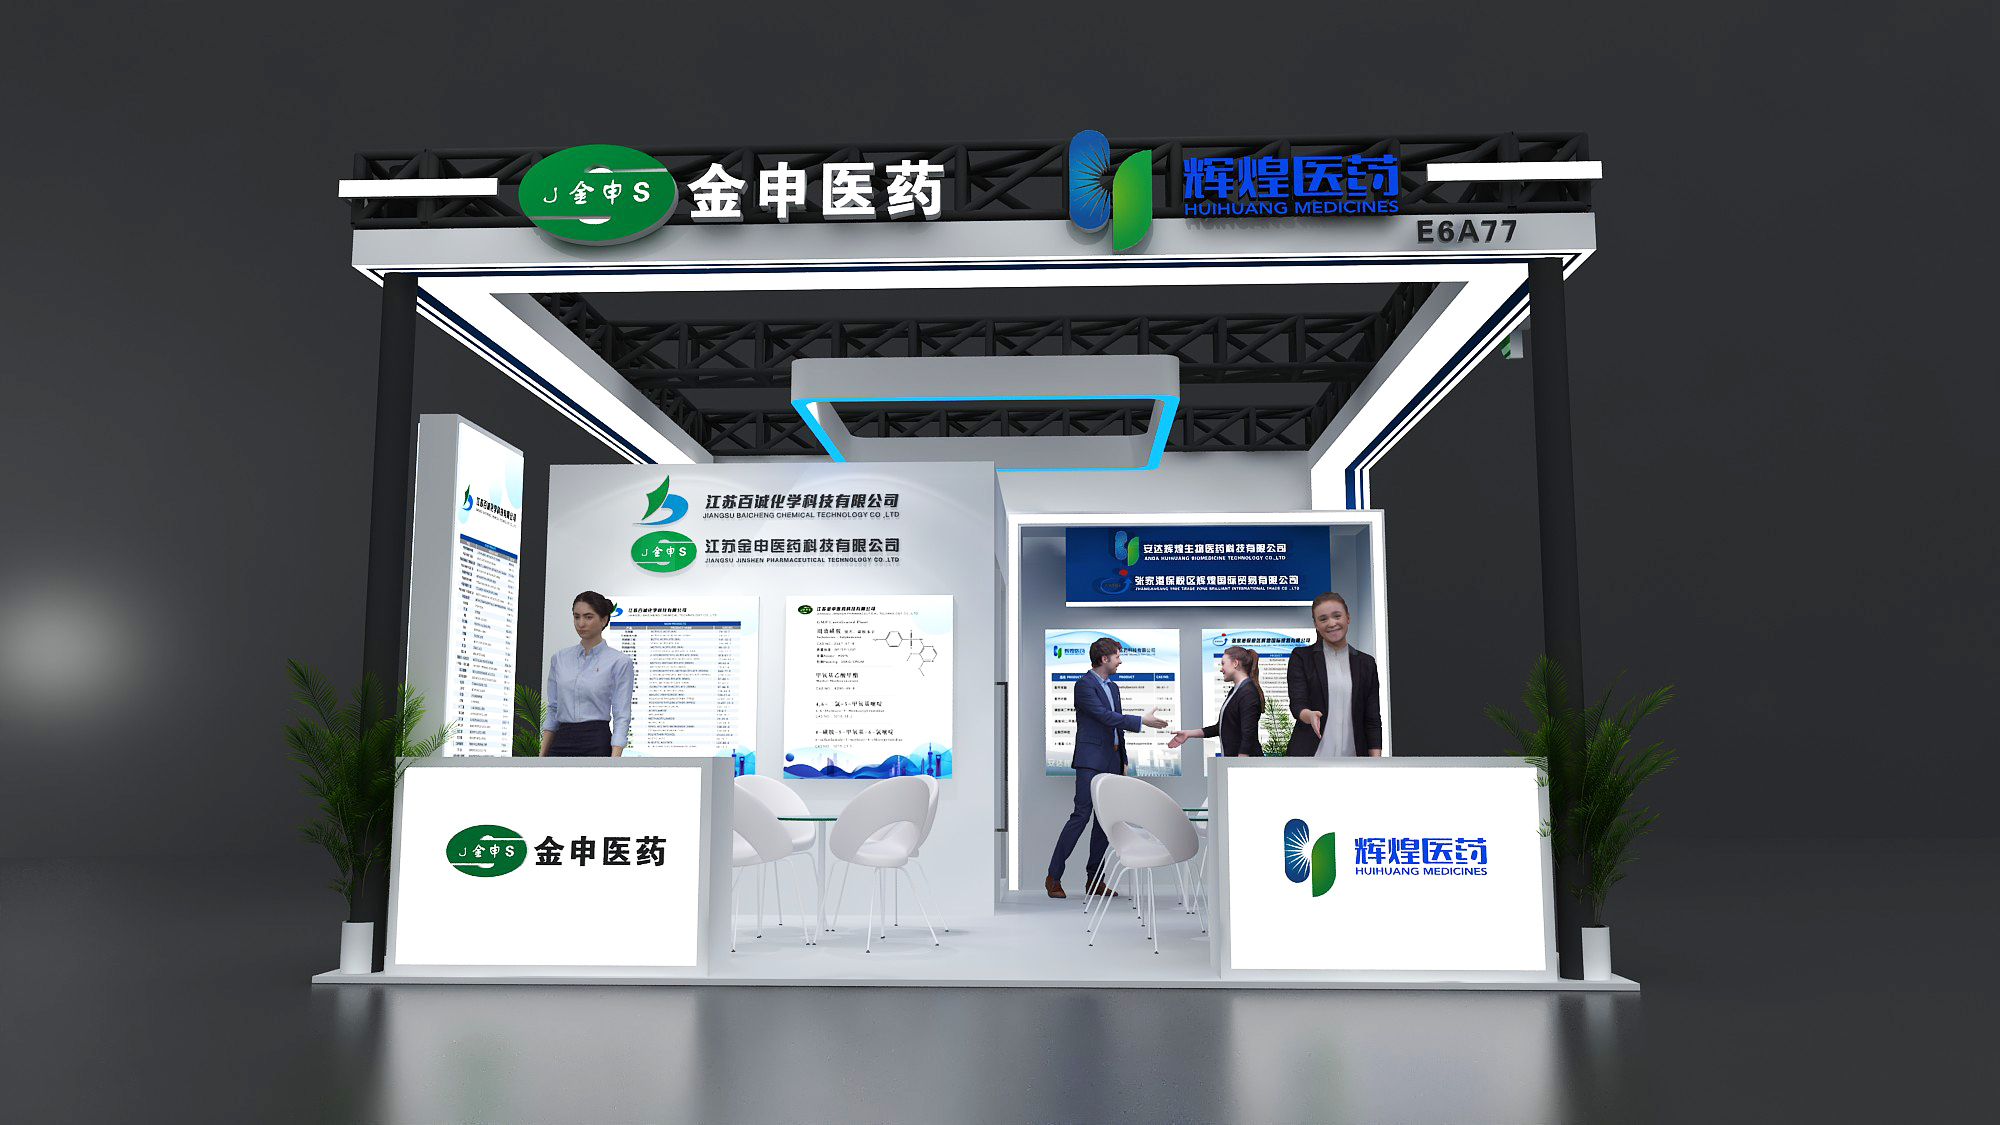
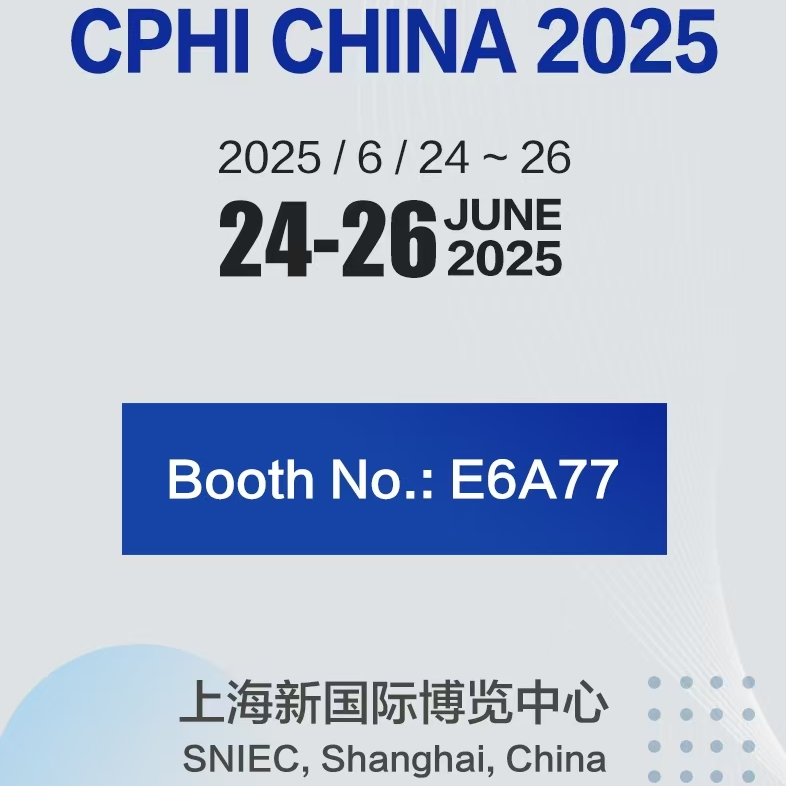
Visit Baicheng Chemical at CPHI China 2025 to Explore Pharmaceutical Solutions (Booth E6A77)

19

Jun

Visit Baicheng Chemical at CPHI China 2025 to Explore Pharmaceutical Solutions (Booth E6A77)

View More
Low-Carbon Footprint Butyl Acrylate (BA) for Global Emulsion Producers

14

Aug

Low-Carbon Footprint Butyl Acrylate (BA) for Global Emulsion Producers

View More
Glacial Acrylic Acid (GAA) Concentrations for Water-Based Resin Makers

14

Aug

Glacial Acrylic Acid (GAA) Concentrations for Water-Based Resin Makers

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

acrylate monomers factory

Advanced Manufacturing Technology and Quality Assurance

Advanced Manufacturing Technology and Quality Assurance

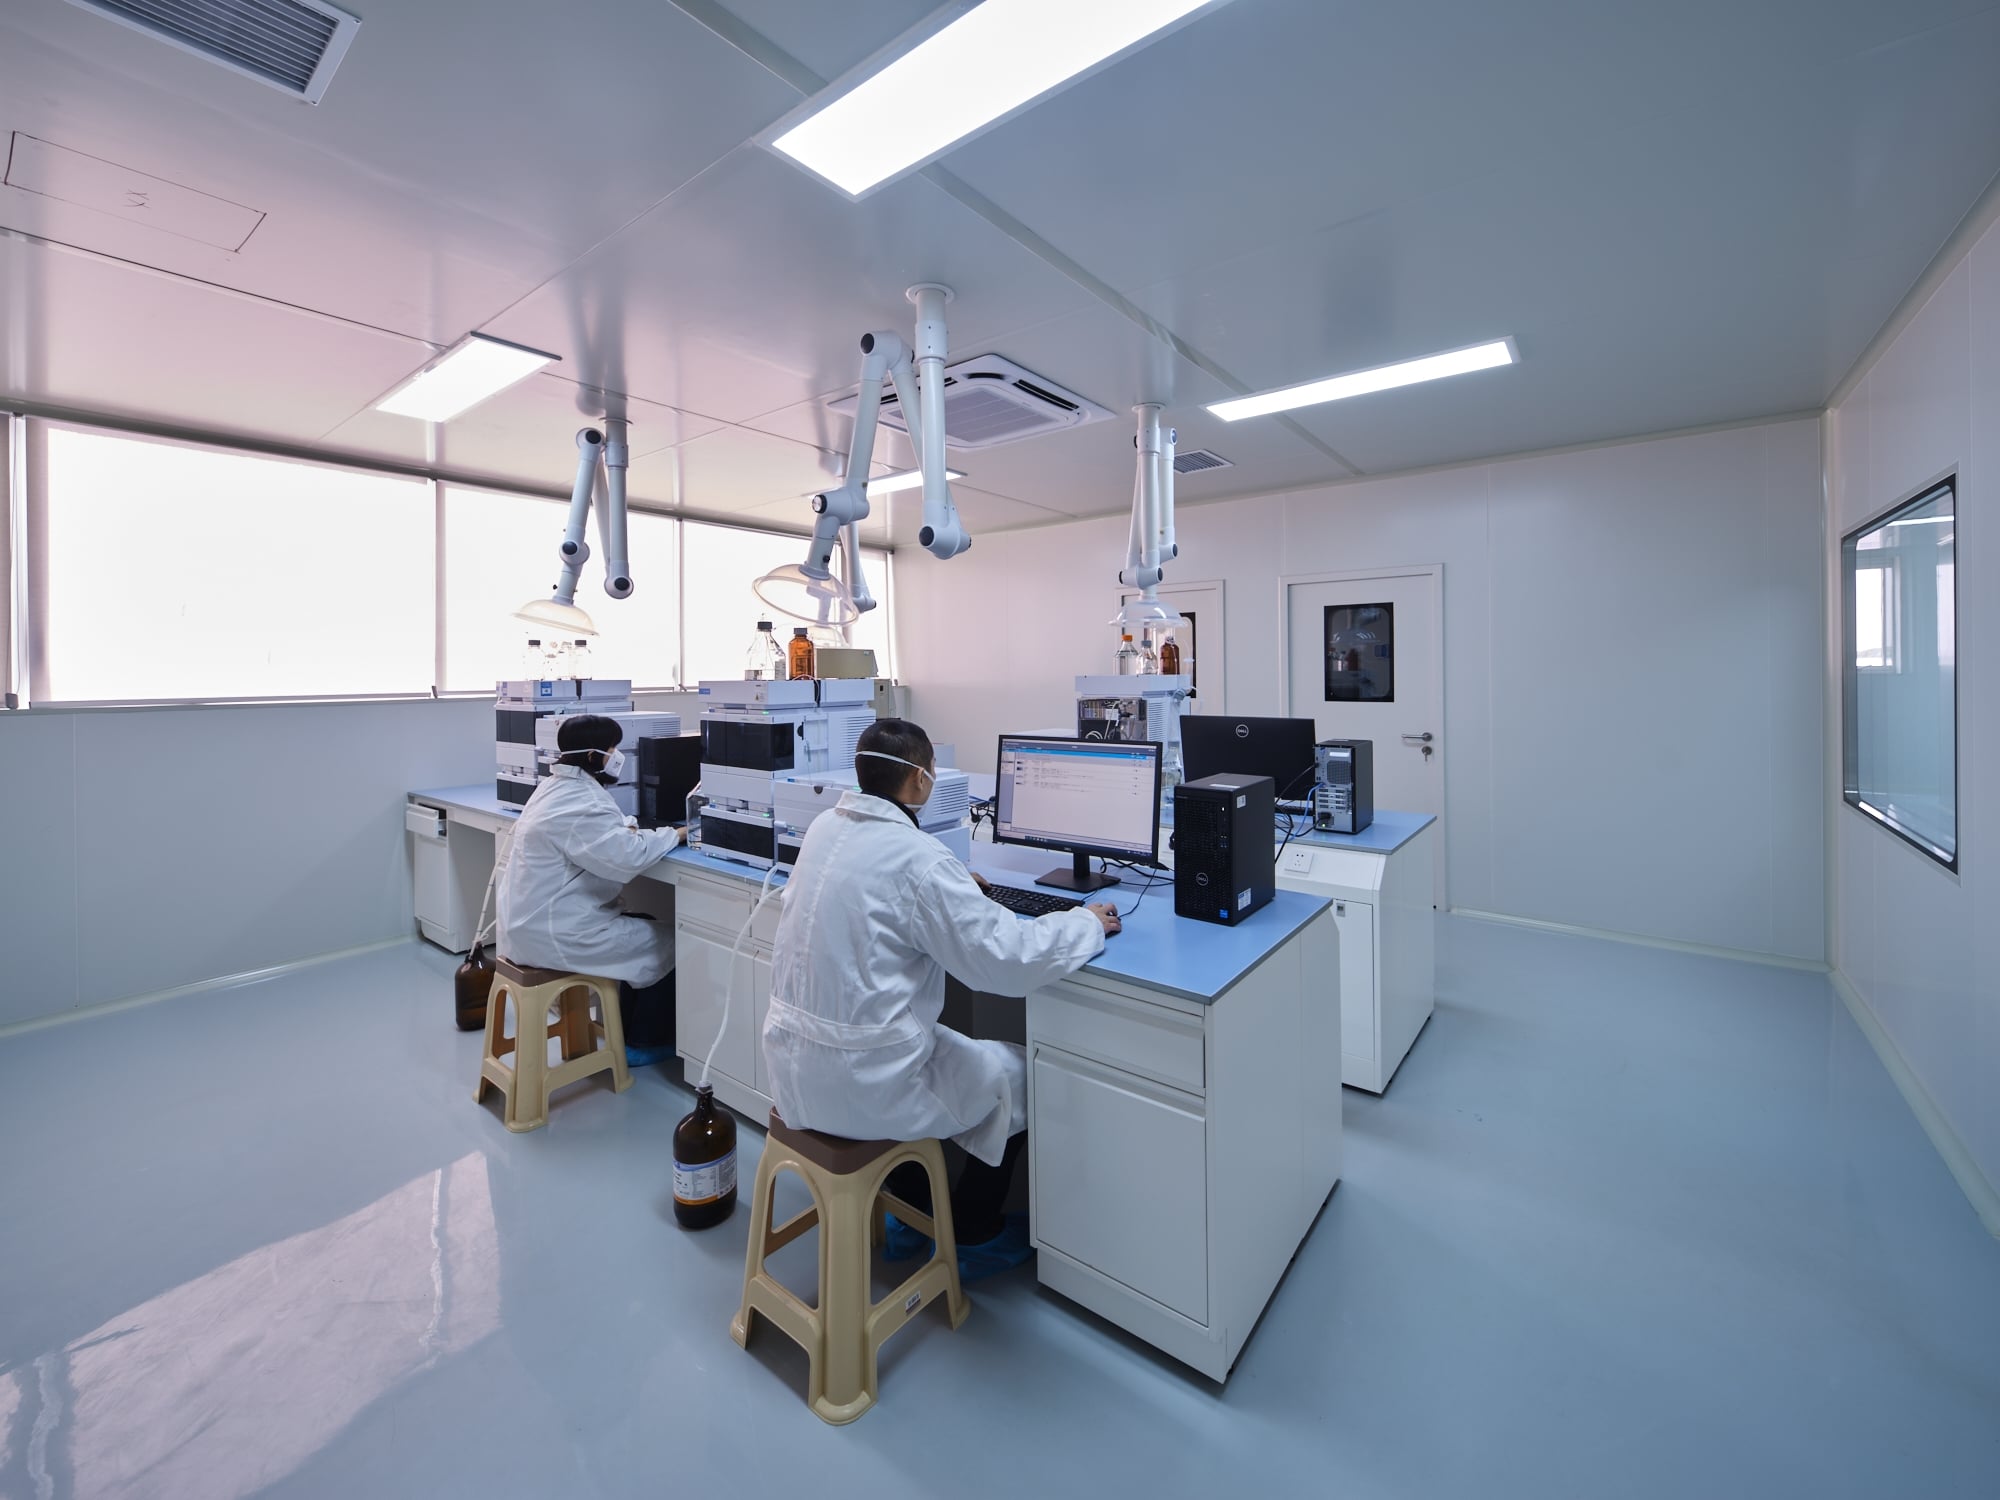
Modern acrylate monomers factory facilities distinguish themselves through state-of-the-art manufacturing technology that guarantees exceptional product quality and consistency. These advanced production systems utilize continuous flow reactors with precise temperature and pressure controls, ensuring optimal reaction conditions that maximize yield while minimizing impurities. Sophisticated analytical equipment including gas chromatography, mass spectrometry, and infrared spectroscopy performs real-time quality monitoring throughout production stages, detecting even trace contaminants before they affect product integrity. Automated process control systems integrate data from multiple sensors to maintain optimal operating parameters, reducing human error and enhancing safety protocols. The quality assurance infrastructure includes dedicated testing laboratories staffed by certified chemists who conduct comprehensive analyses on every production batch, verifying specifications such as purity percentages, moisture content, stabilizer levels, and polymerization inhibitor concentrations. This technological excellence ensures that every shipment from an acrylate monomers factory meets or exceeds customer specifications, providing the reliability essential for critical applications in pharmaceuticals, electronics, automotive components, and high-performance coatings. Investment in cutting-edge technology demonstrates commitment to continuous improvement and positions customers to benefit from innovations that enhance product performance and manufacturing efficiency.
Comprehensive Safety and Environmental Management Systems

Comprehensive Safety and Environmental Management Systems

Safety and environmental stewardship represent fundamental priorities for any responsible acrylate monomers factory, directly benefiting customers through regulatory compliance and sustainable operations. These facilities implement multi-layered safety protocols including advanced fire suppression systems, emergency shutdown mechanisms, personal protective equipment programs, and regular safety training for all personnel handling reactive chemical materials. Environmental management systems address every aspect of production impact, from air emissions control using scrubbers and catalytic converters to wastewater treatment facilities that remove organic compounds before discharge. Sophisticated containment systems prevent accidental releases, while secondary containment structures protect groundwater from potential contamination. Leading factories achieve certifications such as ISO 14001 for environmental management and OHSAS 18001 for occupational health and safety, demonstrating verifiable commitment to responsible operations. These comprehensive systems reduce liability risks for customers by ensuring materials are produced under conditions that meet stringent regulatory requirements across different jurisdictions. The environmental benefits extend to carbon footprint reduction through energy recovery systems, renewable energy integration, and process optimization that minimizes raw material consumption. Customers partnering with environmentally responsible acrylate monomers factory operations strengthen their own sustainability credentials, satisfy stakeholder expectations, and future-proof their supply chains against increasingly strict environmental regulations.
Technical Support and Custom Solution Development

Technical Support and Custom Solution Development

Exceptional customer service distinguishes leading acrylate monomers factory providers through comprehensive technical support and custom solution development capabilities that accelerate your product innovation cycles. Dedicated technical teams with extensive polymer chemistry expertise collaborate with customers to understand specific application challenges, recommend optimal monomer selections, and develop tailored formulations that achieve desired performance characteristics. This consultative approach includes laboratory services for compatibility testing, stability studies, and performance validation using your actual production conditions, eliminating guesswork and reducing development costs. Application engineers provide on-site support during product trials, troubleshooting formulation issues, optimizing processing parameters, and training your personnel on best practices for handling and utilizing acrylate monomers safely and effectively. Custom synthesis capabilities allow the factory to modify standard products or develop entirely new monomer variants that address unique requirements for specialized applications such as UV-curable systems, water-based formulations, or temperature-resistant polymers. Comprehensive technical documentation including safety data sheets, product specifications, application guides, and regulatory compliance certificates streamlines your quality management and accelerates product approvals. This partnership approach transforms the acrylate monomers factory from a mere supplier into a strategic collaborator that contributes intellectual capital, technical resources, and industry insights that enhance your competitive capabilities and expand your market opportunities through innovative product development.
email goToTop